Product Description
Engineered to conquer the most extreme environmental challenges in bulk material handling, our premium HDPE Elevator Bucket is the ultimate solution for facilities operating in harsh climates. As a premier low temperature resistant grain bucket, it is formulated with advanced polymers that maintain exceptional ductility and structural integrity even in freezing conditions. This ensures that the anti aging grain handling bucket will not become brittle, crack, or fail prematurely when exposed to severe winter weather or sub-zero processing environments.
Beyond its impressive thermal resilience, this lightweight grain handling elevator bucket is designed to maximize operational efficiency without compromising on strength. The optimized structural design delivers a high load-bearing capacity, allowing it to transport massive volumes of dense materials with ease. Because of its lightweight nature, this high load bearing food grade bucket significantly reduces the overall rotational mass of your elevator system. This translates directly into decreased energy consumption, lower strain on drive motors, and extended conveyor belt life, making it a highly cost-effective upgrade for modern agricultural and industrial facilities.
Safety and hygiene are paramount in food processing, and our customizable food grade elevator bucket exceeds these rigorous demands. Manufactured from 100% non-toxic, FDA-approved virgin HDPE, it guarantees zero contamination for wheat, corn, rice, and other sensitive agricultural products. The ultra-smooth, non-stick interior surface prevents material buildup and ensures a clean discharge cycle, drastically reducing the need for manual cleaning and minimizing product degradation.
To guarantee a flawless fit for your specific machinery, we offer comprehensive customization services. Whether you require a low temperature resistant customizable bucket with specialized drilling patterns, adjusted hole spacing, or unique dimensional modifications, our team can tailor the product to your exact needs. Upgrade your conveying infrastructure with this anti aging customizable elevator bucket to achieve unmatched durability, superior safety, and long-term economic benefits in any demanding application.

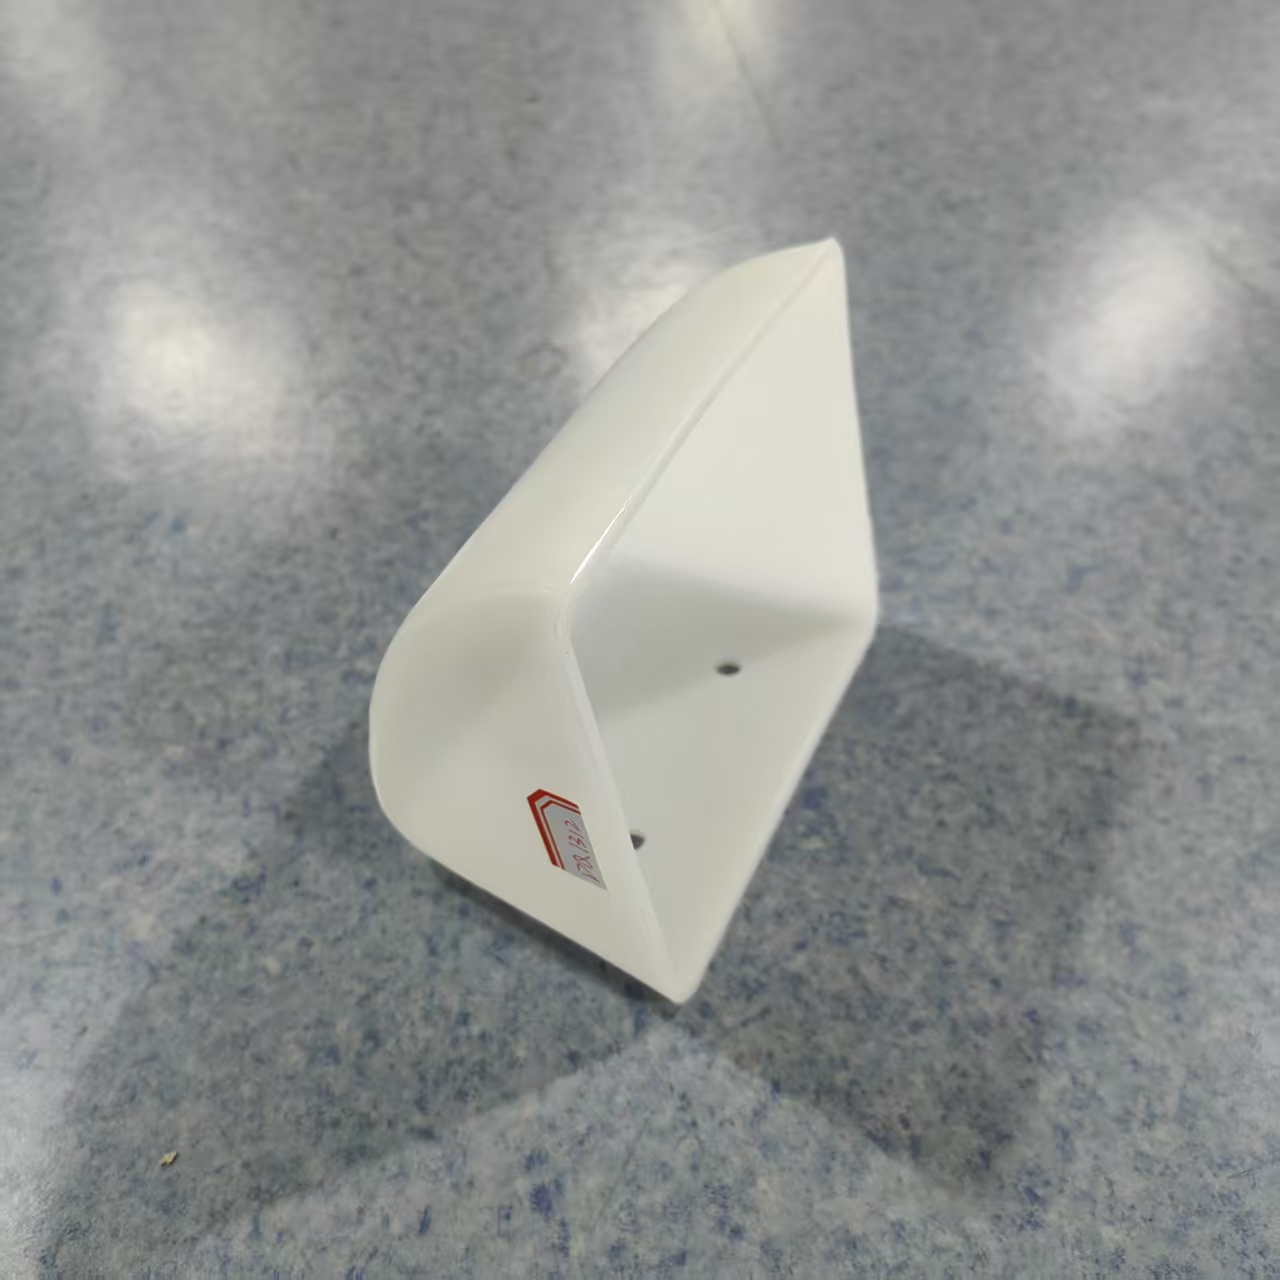
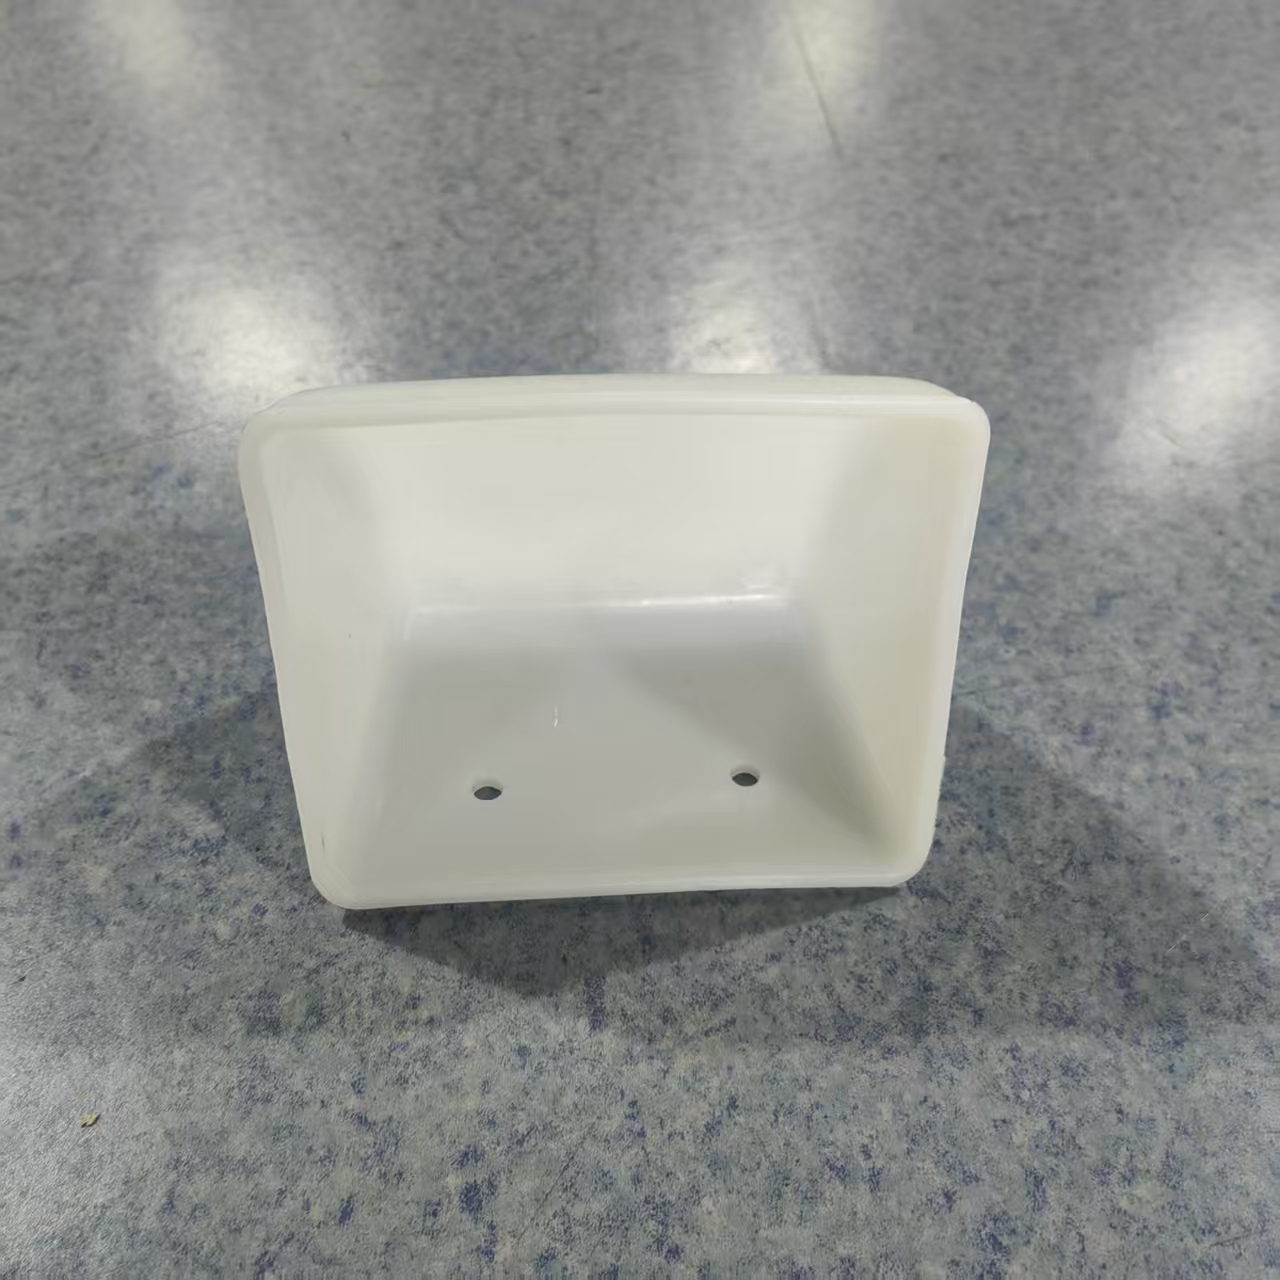
DQ1312
Material: HDPE/Nylon
Bucket Size: 135X117X85 (mm) HDPE / 137X119X87 (mm) Nylon
Holes: 2pcs
Center to Center Distance: 60 mm
Hole Diamater: Φ 7
Water Capacity: 0.61L
Packing: 210pcs/bag (HDPE/Nylon)
Bag Volumn: 950X600X120 mm
Gross Weight: 21.4kg/bag (HDPE)27.6kg/bag (Nylon)
HS code: 843110 0000
Remark:
Jingwei offers custom hole-drilling solutions for elevator buckets, meeting precise size specifications to fit your specific applications perfectly.
FAQ:
Q: Are you manufacturer or trading company?
A: JIANGSU JINGWEI is a leading and professional manufacturer of grain conveying equipment accessories over 15 years in China.
Q: What is your payment term?
A: Our usual payment is 30%TT in advance, 70%TT before shipment (the bill of landing). For small quantity, we also accept other ways after discussion.
Q: Could I buy sample first or small order and is the sample fee refundable?
A: Of course. We accept sample and small order especially for new customers and of course the sample fee will be refundable when order confirmed.
Q: When can delivery from ordering?
A: The delivery time depends on the quantity you ordered, generally about 5-45 days after deposit of payment.
Q: What is the quality of your products?
A: Quality is our corporate culture, we regard product quality as the life of our company. We have achieved a lot of certifications to meet customs requirements. As a factory, we can control all processes of production 100% and every single product will be tested qualified before shipping.
Q: How long is the warranty of your product?
A: Our warranty period is usually one year. But the warranty period can be extended after discussion and agreement.


